
What Can Go Wrong with BESS Punch List Handover?
Your BESS project is almost complete. The finish line is in sight. But the final handover punch list reveals unexpected problems, delaying startup and creating commercial risk.
What goes wrong is a failure to treat factory proof, installed proof, and operational acceptance as three separate, mandatory gates. Gaps between these stages can hide serious issues with reliability, safety, or commercial value that only surface after you have taken over the asset.
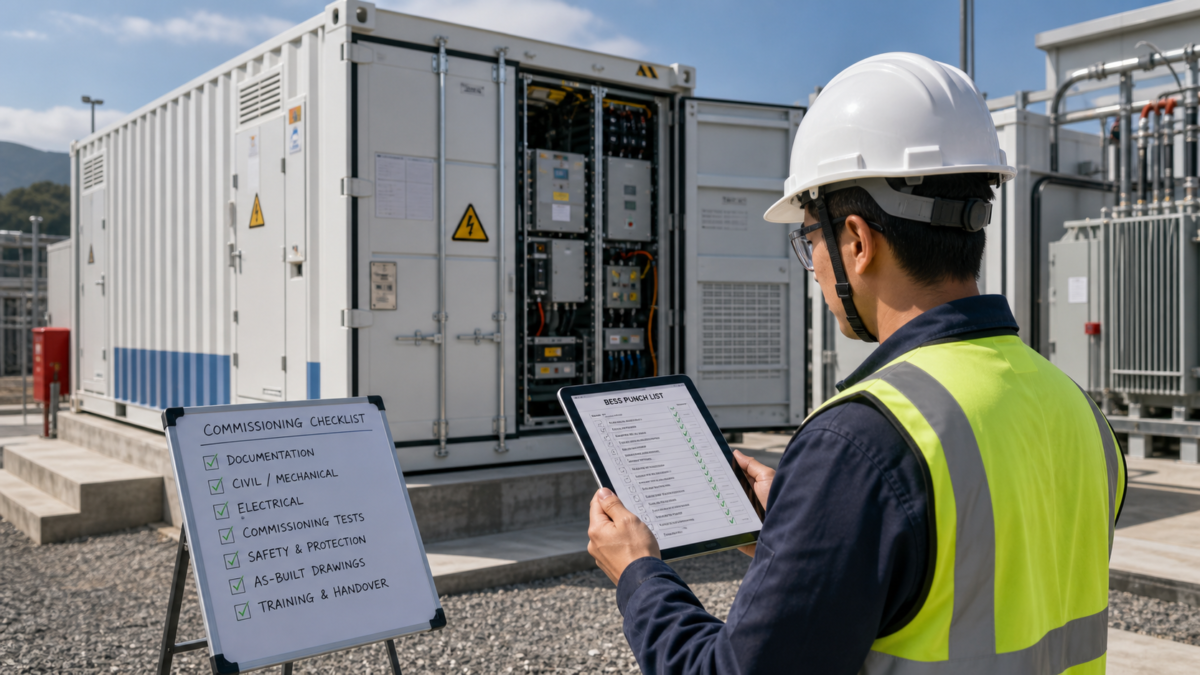
I've learned to see the punch list not as a final task, but as a critical design and operating decision. It's the moment where paper promises meet physical reality. If the evidence isn't there, the promise isn't real. The details I'm about to share are exactly what I would demand before signing off on a project or using a supplier's claims in an RFQ. Let's look at where the process can fail and how to protect your investment.
Why BESS Punch List Handover Is Harder Than It Looks?
You have the factory acceptance test (FAT) report, and it's perfect. But on-site, the equipment doesn't fit the foundation, or interfaces don't align. Why does this happen?
BESS handover is difficult because it combines the separate worlds of manufacturing, logistics, civil engineering, and electrical integration. A component that passes tests in a controlled factory environment is not guaranteed to perform correctly after being shipped, craned into place, and connected to other systems on-site.
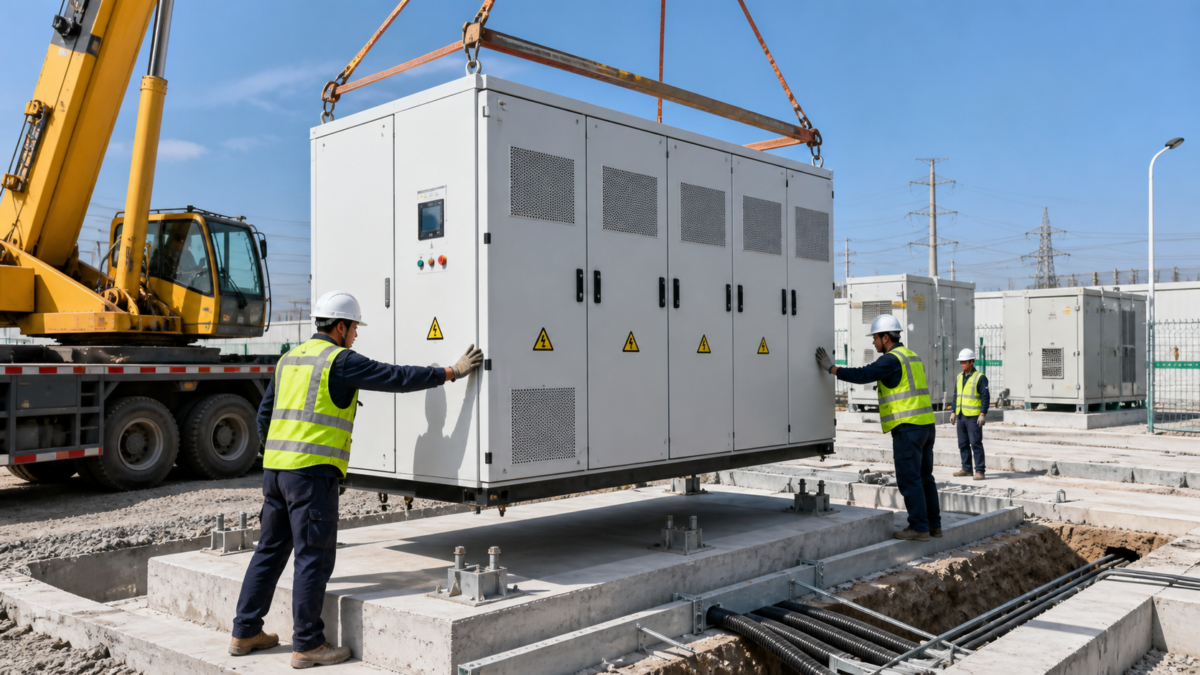
I once worked on a project where the BESS containers arrived with perfect FAT reports. The problem was, the civil works contractor poured the concrete foundations based on an older drawing revision. The anchor bolts were off by 50 millimeters. It was a simple error that caused weeks of delays for rework and re-inspection. This taught me that handover isn't one event; it’s a series of gates. You must verify each one independently. What passes in the factory is only the first step. Proving it's installed correctly is the second. And proving it operates as a complete system is the third and most important. Ignoring the gaps between these stages is a recipe for failure.
The Three Gates of Project Proof
To make this clear, I’ve broken down the key differences between these gates. Each one requires a different type of proof.
| Project Aspect | Gate 1: Factory Proof (FAT) | Gate 2: Installed Proof (SAT) | Gate 3: Operational Acceptance |
|---|---|---|---|
| Interface Matrix | Component-level connections are simulated. Communication ports are tested individually. | Physical cables are connected. Point-to-point communication is verified. | The entire system communicates and operates under load. Data is logged correctly in the EMS. |
| Foundation | Not applicable. The unit is on a factory floor. | Unit is placed, leveled, and bolted. Bolt torque is verified and marked. | No excessive vibration during operation. Long-term stability is confirmed after thermal cycling. |
| Packing & Logistics | Unit is packed according to a shipping plan. | Packing is removed. Unit is inspected for any shipping damage before installation. | Not applicable, but damage found later points to a failure at this stage. |
| Document Register | FAT reports, manuals, and packing lists are issued. | Installation reports, test records, and red-line drawings are created. | Final as-built drawings, signed commissioning sheets, and training records are handed over. |
The Site Data Needed to Evaluate BESS Punch List Handover?
The EPC tells you the system is commissioned and ready. But how do you actually know? You need objective proof, not just someone's word that the job is done.
To properly evaluate a handover, you need a file of verifiable evidence. This must include signed test sheets with real data, time-stamped photos of key installation steps, calibration certificates for all test instruments, records of closed non-conformance reports, and final as-built drawings.
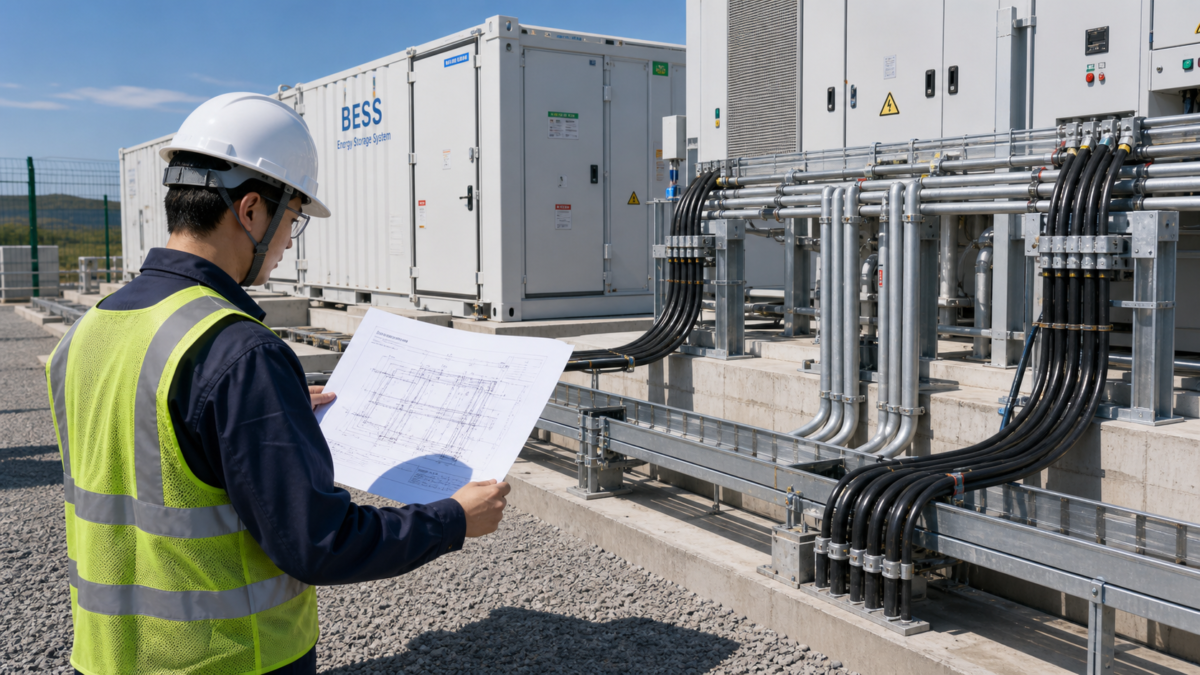
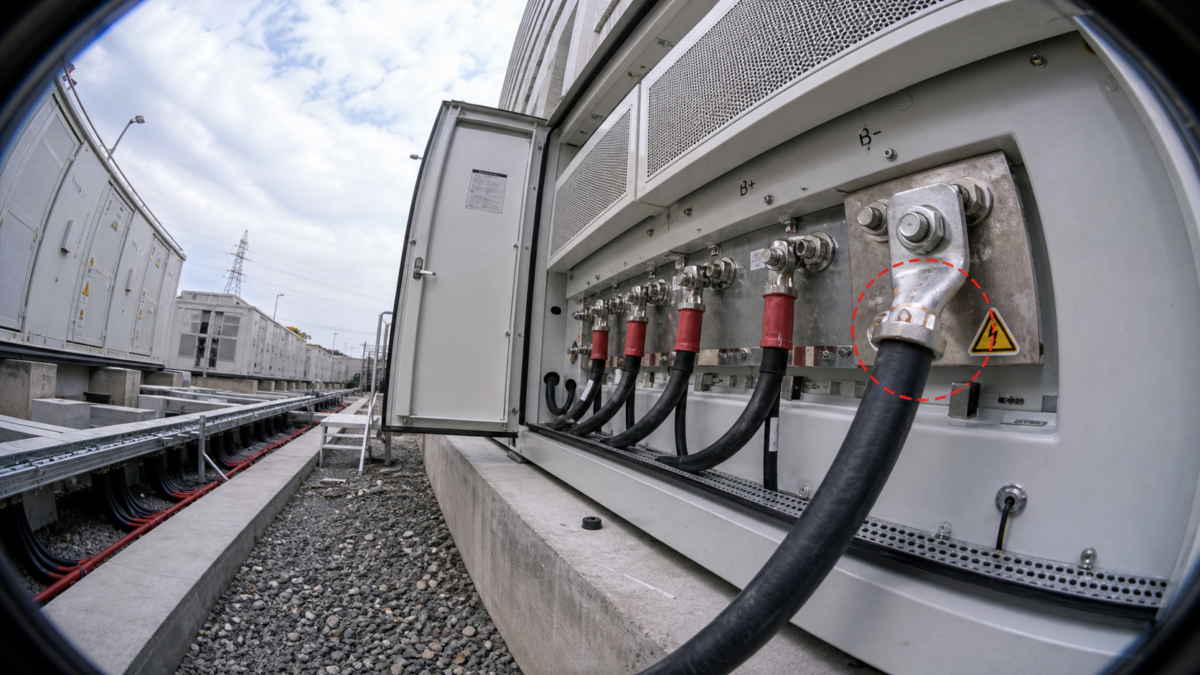
This evidence trail is non-negotiable. I insist on seeing it for every project. For example, a signed test sheet is good, but a test sheet that includes the serial number of the calibrated torque wrench used on the DC busbars is much better. It proves the work was done with the right tools to the right specification. Photos are also critical. A picture of a correctly terminated high-voltage cable, taken before the heat shrink is applied, provides confidence that you can’t get from a simple checkbox. This data isn't just for the punch list; it becomes the baseline for the asset’s entire operational life. It's what your maintenance teams will rely on for years to come. Without this detailed, project-specific record, you are essentially accepting the system blind, and any future problems will be much harder and more expensive to diagnose and fix.
Which BESS Punch List Handover Assumptions Distort the Result?
You assume a "certified" product will work flawlessly. You assume the contractor understands every detail of the design. These common assumptions can hide major risks that emerge after handover.
The most dangerous assumption is that "factory passed" means "site ready." Other distorting assumptions include believing generic manuals apply perfectly to your unique site, that all installers are equally skilled, or that small on-site changes won't impact performance, safety, or warranty.
I remember a project in a high-altitude location. The equipment was specified and factory-tested at sea level. The project team assumed the standard cooling system would be sufficient. However, the thinner air at altitude reduced the cooling efficiency, causing the system to de-rate on hot days and fail to meet its commercial obligations. The problem wasn't the equipment; it was the flawed assumption that the operating environment wouldn't matter. This is why I always treat handover as a design and operating decision. We have to make all assumptions visible and test them. For any given project, I would want to see the specific manufacturing capabilities of a supplier like Moletong and the disclosed site capabilities of the EPC. This grounds the project in reality and moves us away from dangerous assumptions that can cost millions in lost revenue or lead to unsafe operating conditions.
A Practical BESS Punch List Handover Selection Checklist?
You need a simple system to track everything. A good checklist helps you manage the details, demand the right evidence, and make sure nothing is forgotten during the busy handover phase.
A practical checklist moves beyond simple checkmarks. It should be structured by discipline—Documentation, Civil/Mechanical, Electrical, and Commissioning. Crucially, each line item must require specific, tangible evidence like a photo, a signed report, a data log, or a measurement record.
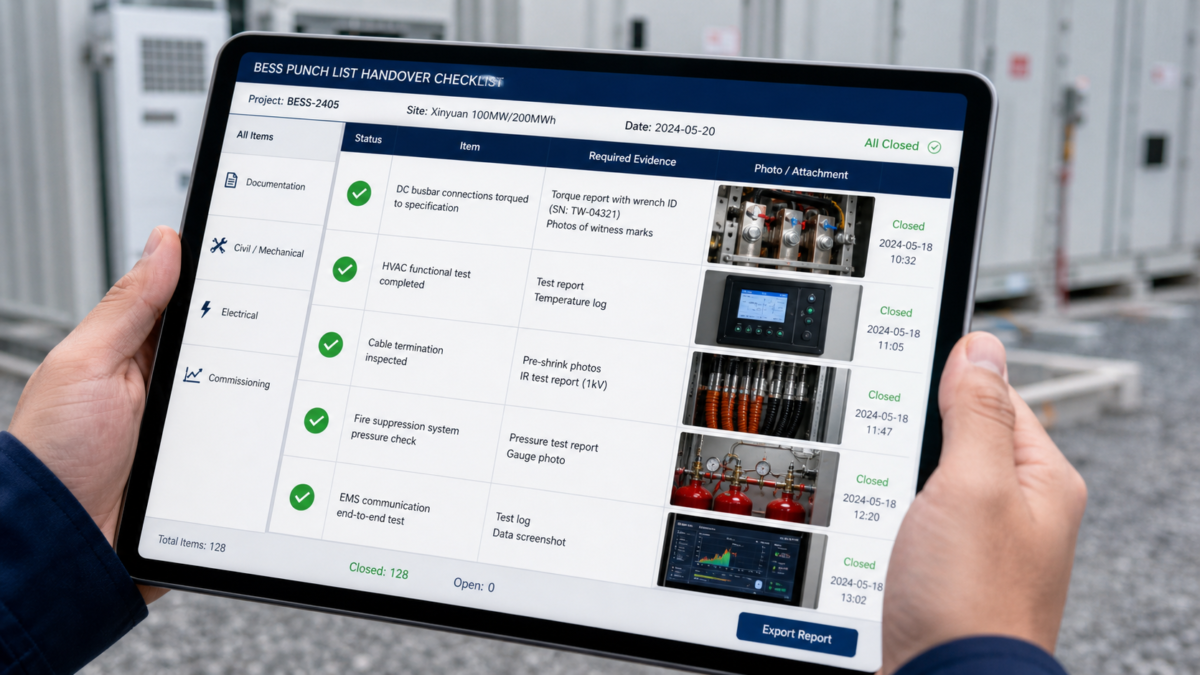
A simple "pass/fail" isn't enough information. Your checklist should be an evidence-gathering tool. For instance, instead of an item that says "Busbar connections checked," it should say, "All DC busbar connections torqued to [X] Nm." The required proof would be: "Torque report log with calibrated wrench ID and photos of witness marks on each bolt." This level of detail removes ambiguity and creates a powerful, auditable record. It also forces the installation team to perform the work correctly because they know what proof they need to provide. Finally, every handover package I accept must include a short, clear table of assumptions. This shows transparency about the conditions under which the system was tested, such as grid stability, ambient temperature, and state-of-charge levels. This is the level of detail I need before I can trust a handover conclusion.
Conclusion
Treat BESS handover as a crucial project gate, not a paper-pushing exercise. Demand objective, verifiable evidence at every step to protect your asset's safety, reliability, and long-term value.
Leave a Reply